Long-Head Casing
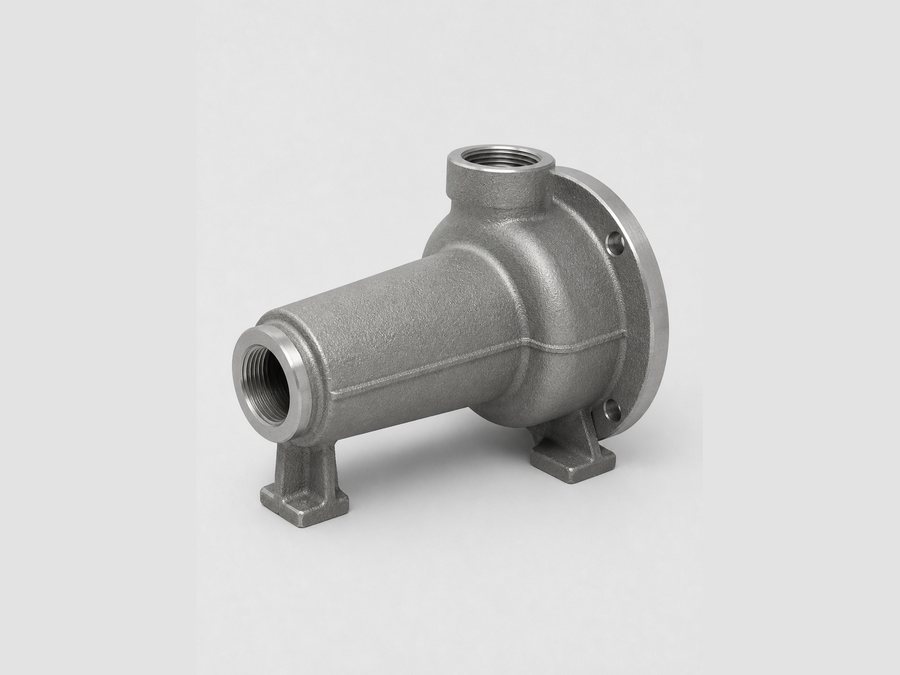
An extended nose barrel, for the higher head duty.
The barrel ahead of the volute is longer, which leaves room for a larger impeller eye and a longer suction passage. That is what buys the extra head — and it is why a long-head and a short-head body are different patterns rather than the same casting cut to length.
Long and relatively thin is the harder shape to pour. The metal has to run the full length of the barrel before it starts to freeze, and the air it displaces has to get out at the far end. Both are gating questions, decided before the first mould is made.
| Casting process | Vertical-line sand moulding on two lines (national patent) |
| Materials | Grey iron · ductile iron · WCB carbon steel · CF8M stainless |
| Machined features | Suction bore and register · joint face and bolt circle · discharge flange · foot |
| Minimum order | 100 pieces |
| Certification | EN 10204 3.1 per heat, spectrometer results |
| Source of geometry | Your drawing, 3D file or a worn sample |
What Is Difficult About This One
Every casting has one or two features that decide whether the batch repeats. On this part they are these.
Long draw needs consistent taper
Draft has to hold all the way down the barrel or the mould tears on the way off. On a long part, a taper that is fine at the top is not automatically fine at the bottom.
Fill before it freezes
Pouring temperature and gate area are set by the length of the run, not by the weight of the casting. This is where a long-head body differs most from a compact one.
Vent the far end
Air trapped at the nose gives blowholes in exactly the section that has to hold pressure. Vents go in the pattern.
Alloy Options
The same geometry is a different part in three different plants. Chloride content, abrasion and temperature drive the choice — not the name of the fluid.
| Alloy | Grade | When it is the right choice |
|---|---|---|
| Grey iron | HT200 / HT250 | Default for water duty. Damps vibration, machines easily, lowest cost. |
| Ductile iron | QT450 / QT500 | When the duty is cyclic or the part takes shock. Tougher than grey. |
| WCB carbon steel | ASTM A216 WCB | Higher strength, weldable. For pressure-bearing bodies. |
| CF8M stainless | ASTM A743 CF8M | Chloride and corrosion duty — the cast equivalent of 316. |
What to Send Us
These are the ones specific to this part. A drawing, a 3D file or the worn original covers all of them at once.
| Item | Why it matters |
|---|---|
| Barrel length and suction bore | The two dimensions that make it a long-head rather than a short-head |
| Head duty | It tells us which body in the family you actually need |
| Mounting foot pitch | Long-head and short-head bodies rarely share one |
Others in Pump Casings & Volutes
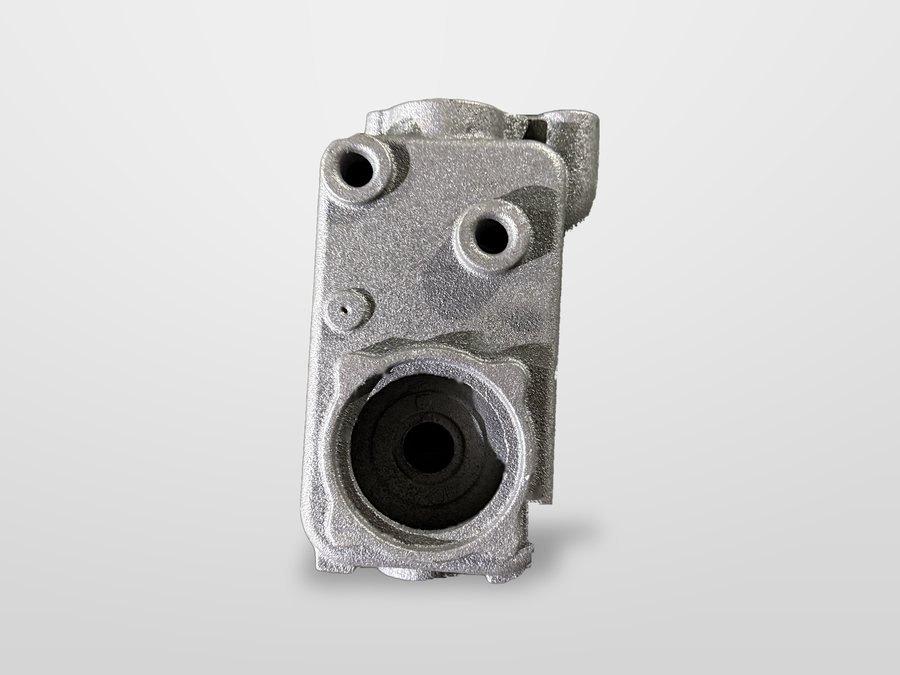
Square Casing
A squared outer shell for booster sets where the footprint is fixed.
View ›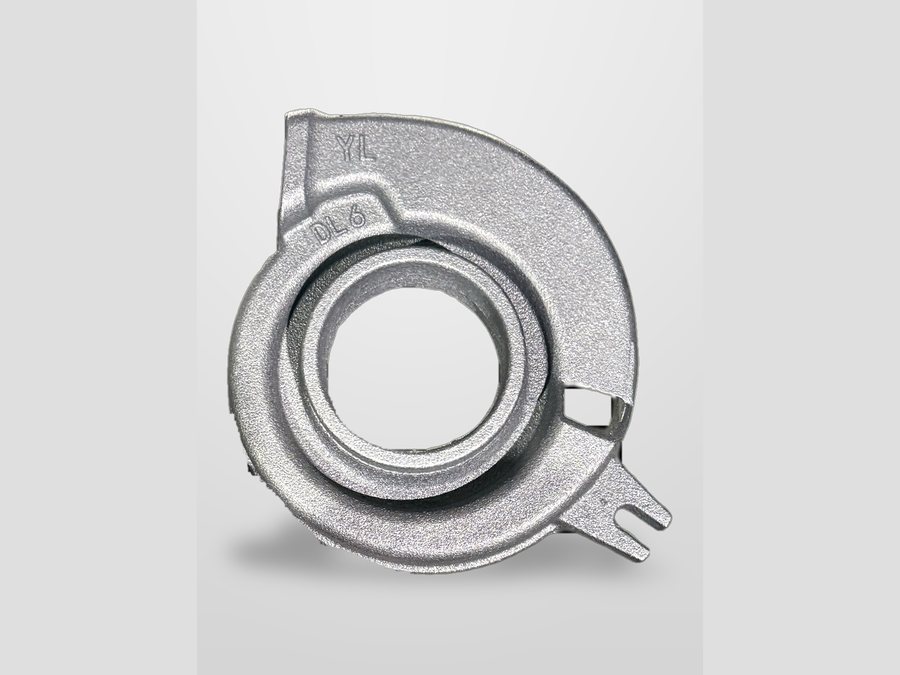
Volute Casing
The spiral scroll, cast to the original profile.
View ›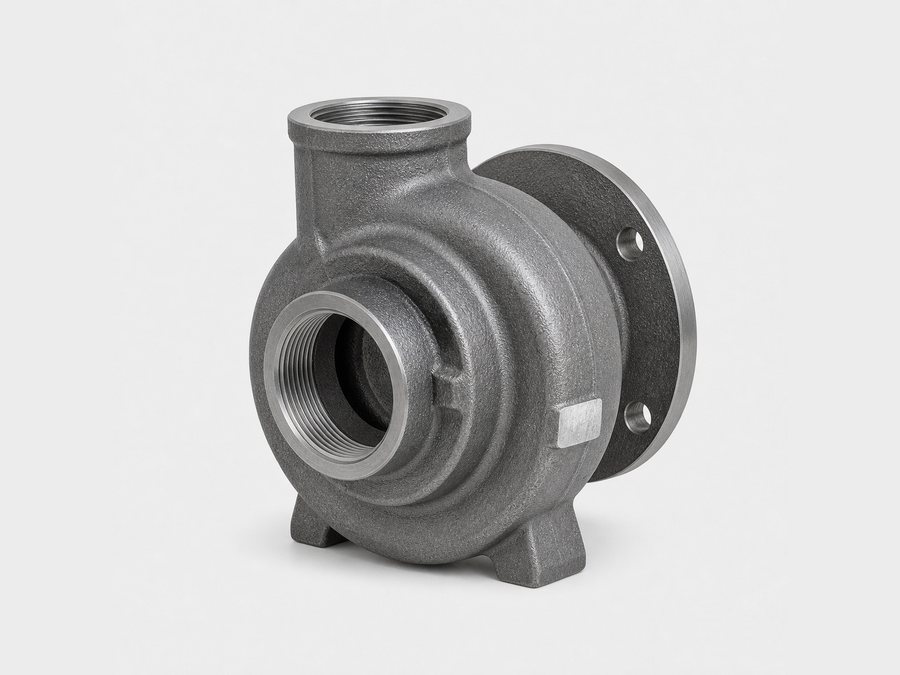
Short-Head Casing
The compact body: lower head duty, shorter overall length.
View ›
Pump Cover
The mating half, machined against the casing it closes.
View ›
Inlet / Outlet Flanges
The connection castings — threaded ports and bolted flange faces.
View ›
Jet Pump Casing
Self-priming jet casing with a threaded port boss
View ›