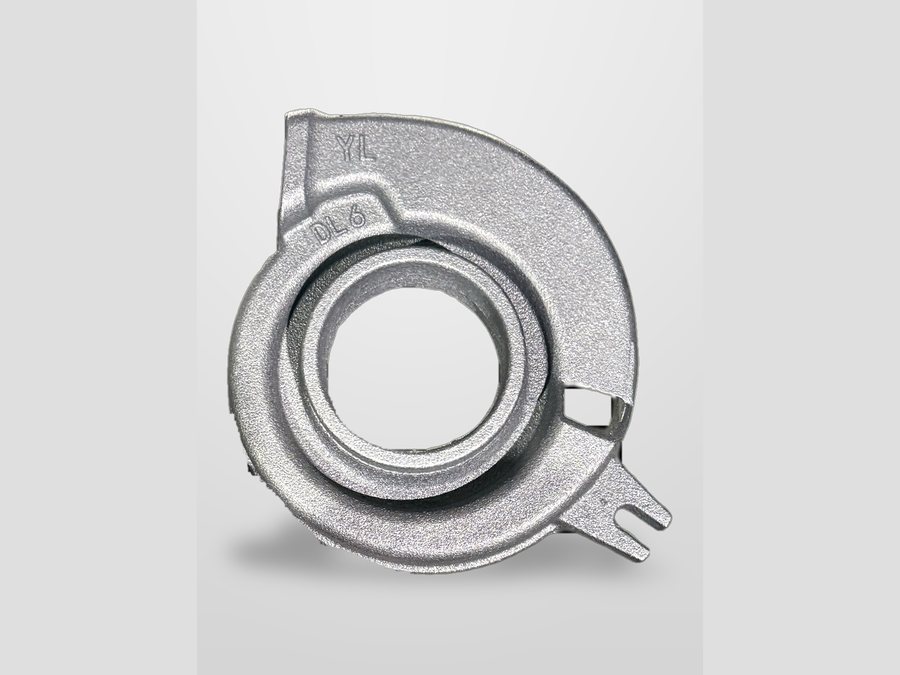
Volute Casing
The spiral scroll, cast to the original profile.
The volute is not a decorative shape. Its cross-section grows along the spiral so that velocity stays roughly constant as flow is collected off the impeller. Change that taper and the pump still runs, but the duty point moves and efficiency drops — usually several points, and always in the wrong direction.
On aftermarket work we reconstruct the profile rather than tracing the worn one. An eroded volute is wider than it left the factory; copying it would build the wear into the new part. Where a dimension came off the sample rather than a drawing, we say so on the quotation.
| Casting process | Vertical-line sand moulding on two lines (national patent) |
| Materials | Grey iron · ductile iron · WCB carbon steel · CF8M stainless |
| Machined features | Joint face and bolt circle · suction and discharge flanges · register bore |
| Minimum order | 100 pieces |
| Certification | EN 10204 3.1 per heat, spectrometer results |
| Source of geometry | Your drawing, 3D file or a worn sample |
What Is Difficult About This One
Every casting has one or two features that decide whether the batch repeats. On this part they are these.
The profile is the part
Everything else on a volute is ordinary casting work. The spiral is where the value is, and it lives entirely in the core box.
Section grows along the spiral
Feeding has to follow that growth, so the thick end near the discharge solidifies last. Feed it the other way round and the shrinkage lands in the throat.
The cutwater is the thin bit
Where the spiral meets the discharge, the wall is at its thinnest and the metal has already travelled furthest. It is the first place to check on a first article.
Alloy Options
The same geometry is a different part in three different plants. Chloride content, abrasion and temperature drive the choice — not the name of the fluid.
| Alloy | Grade | When it is the right choice |
|---|---|---|
| Grey iron | HT200 / HT250 | Default for water duty. Damps vibration, machines easily, lowest cost. |
| Ductile iron | QT450 / QT500 | When the duty is cyclic or the part takes shock. Tougher than grey. |
| WCB carbon steel | ASTM A216 WCB | Higher strength, weldable. For pressure-bearing bodies. |
| CF8M stainless | ASTM A743 CF8M | Chloride and corrosion duty — the cast equivalent of 316. |
What to Send Us
These are the ones specific to this part. A drawing, a 3D file or the worn original covers all of them at once.
| Item | Why it matters |
|---|---|
| Pump make and model | Or the worn casing itself — either lets us reconstruct the profile |
| Impeller diameter | Sets the volute throat and the register that holds it central |
| Flange standard | PN/ANSI rating, or a drawing of what it bolts to |
Others in Pump Casings & Volutes
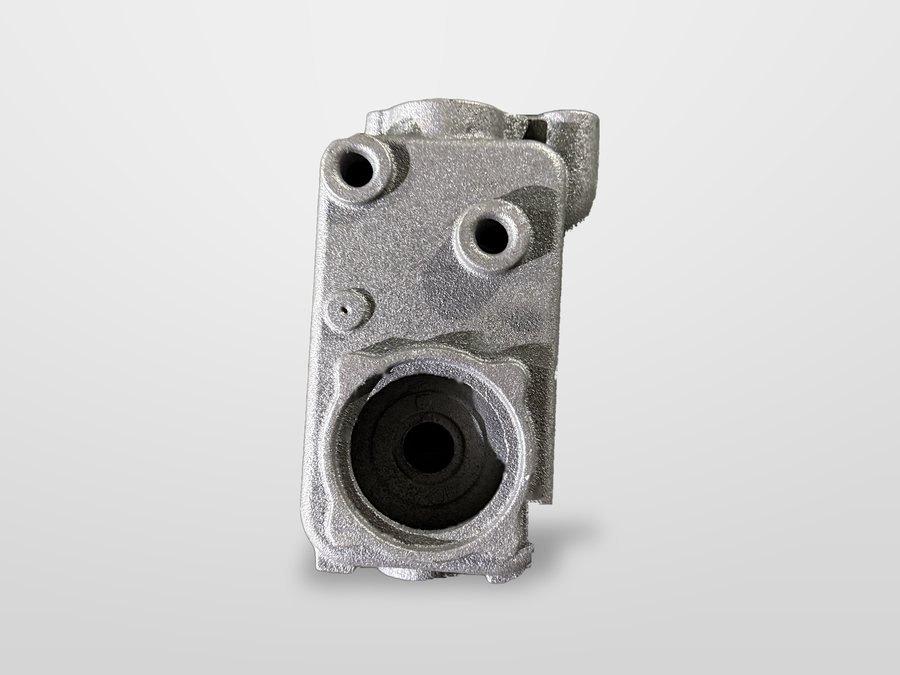
Square Casing
A squared outer shell for booster sets where the footprint is fixed.
View ›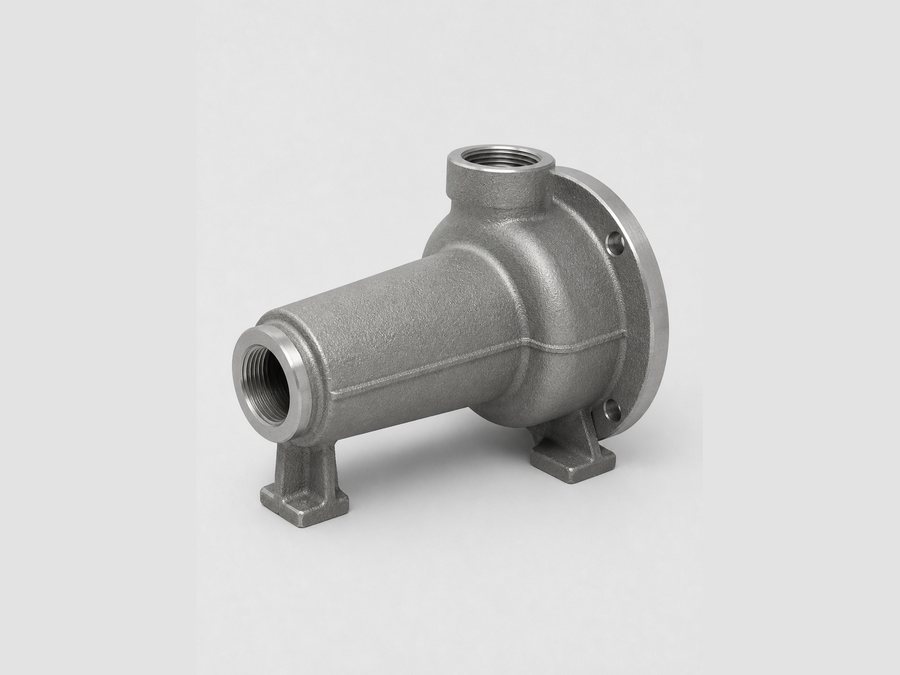
Long-Head Casing
An extended nose barrel, for the higher head duty.
View ›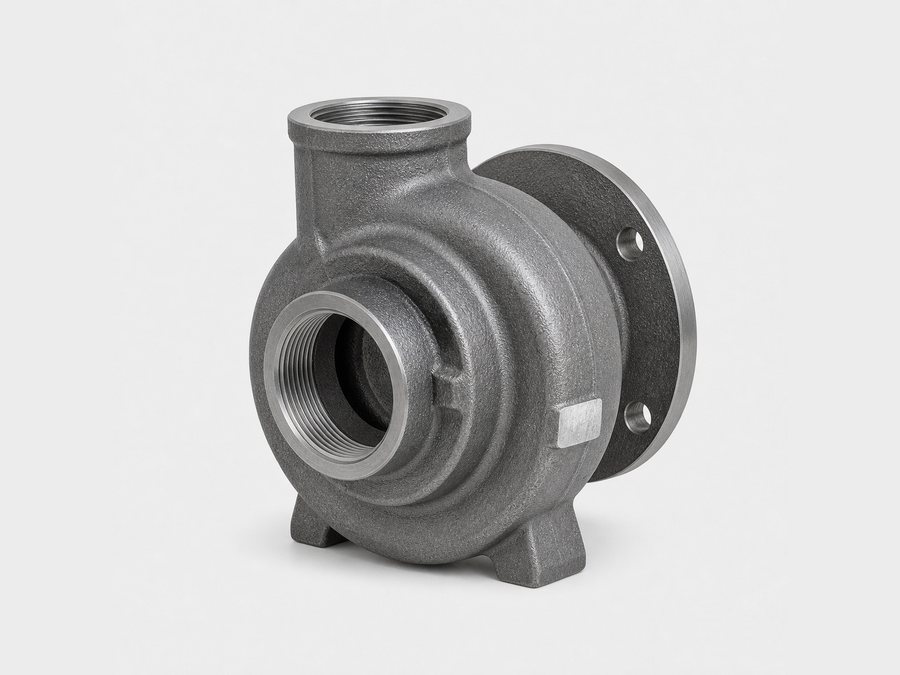
Short-Head Casing
The compact body: lower head duty, shorter overall length.
View ›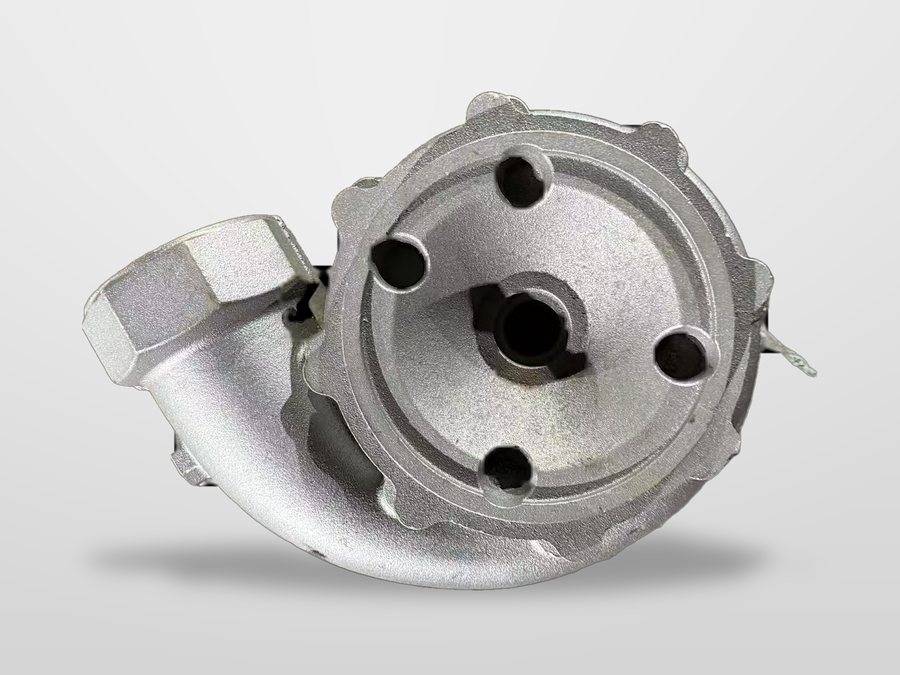
Pump Cover
The mating half, machined against the casing it closes.
View ›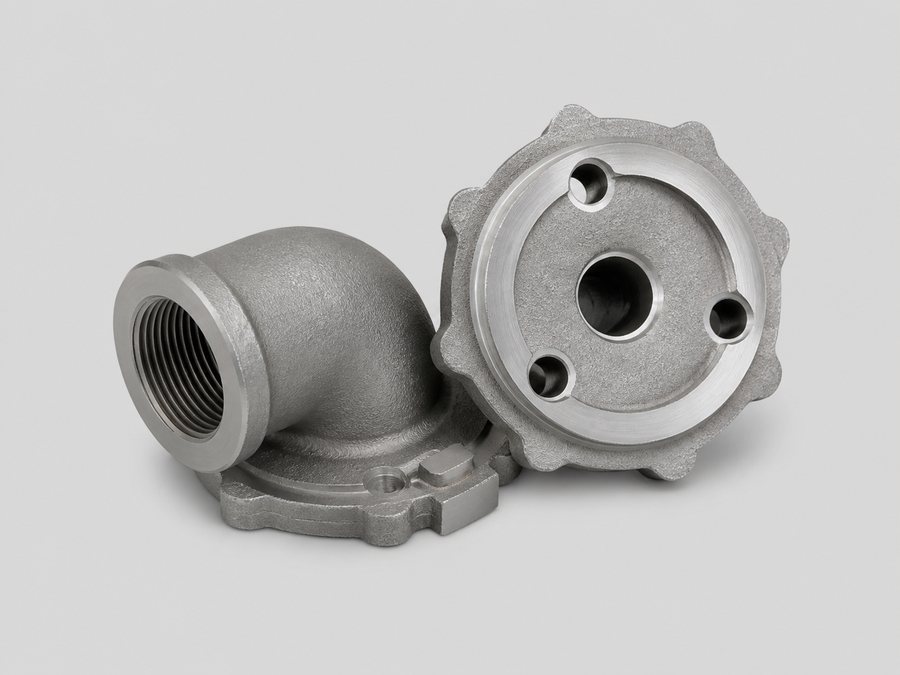
Inlet / Outlet Flanges
The connection castings — threaded ports and bolted flange faces.
View ›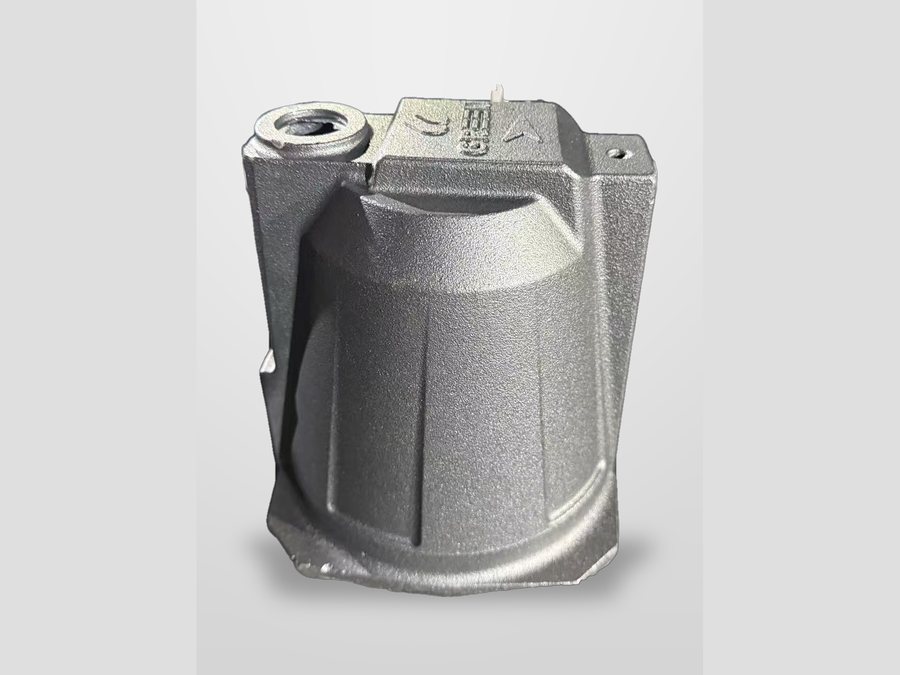
Jet Pump Casing
Self-priming jet casing with a threaded port boss
View ›