200W Pump Casing
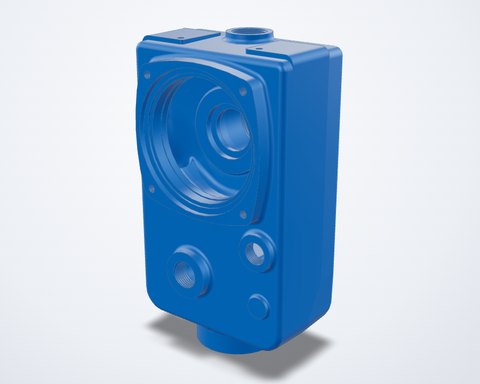
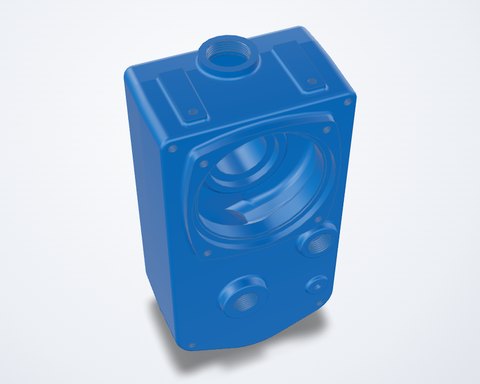
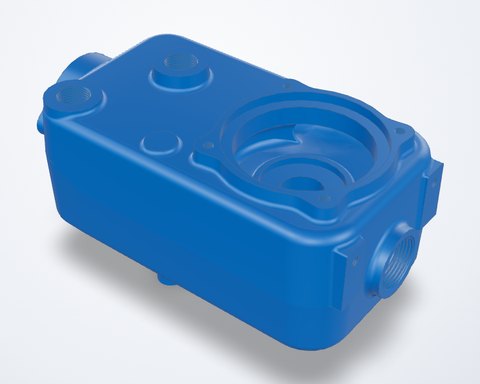
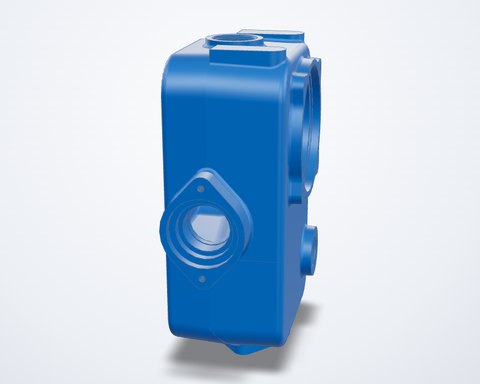
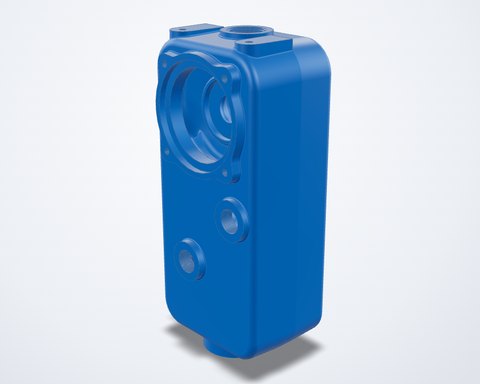
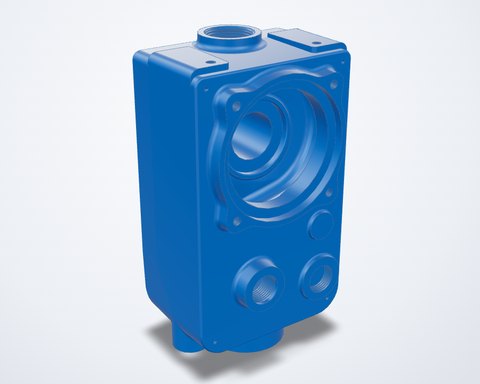
A vertical casing for the 200 W frame: impeller chamber on the front face, a threaded port on top between two raised pads, and the mounting foot coming straight off the bottom of the body.
The whole envelope is 109 × 80 × 167 mm and it is one casting — chamber, port boss and foot together. Nothing is welded on afterwards. That is the point of casting it: a welded foot is a fatigue crack waiting for the first pump that runs slightly out of balance.
The front face carries a stepped impeller chamber on a four-bolt circle, with two smaller cored ports alongside it. Those steps are what set the impeller clearance, so they are the faces we machine and the ones we measure on the first article.
| Envelope | 108.8 × 79.8 × 166.8 mm |
| Cast volume | 269.8 cm³ |
| Weight, grey iron | approx. 1.94 kg as-cast |
| Casting process | Vertical-line sand moulding on two lines (national patent) |
| Materials | Grey iron · ductile iron · WCB carbon steel · CF8M stainless |
| Machined features | Front chamber steps and bolt circle · top port thread and pad faces · foot underside |
| Minimum order | 100 pieces |
| Certification | EN 10204 3.1 per heat, spectrometer results |
| Source of geometry | Your drawing, 3D file or a worn sample |
What Is Difficult About This One
Every casting has one or two features that decide whether the batch repeats. On this part they are these.
Chamber is the main core
The stepped bore through the front face is cored, not drilled. Core print location decides the wall thickness behind the chamber, which is the thinnest section in the part.
Foot and body on one parting line
The foot sits at the bottom of the same draw, so the whole casting comes off the line in one pull. No loose pieces, which is what keeps a 100-off batch repeatable.
Top pads machined flat
The two raised pads either side of the top port are the mating faces. They are cast proud and skimmed, so the port lands square whatever the mould does.
Alloy Options
The same geometry is a different part in three different plants. Chloride content, abrasion and temperature drive the choice — not the name of the fluid.
| Alloy | Grade | When it is the right choice |
|---|---|---|
| Grey iron | HT200 / HT250 | Default for water duty. Damps vibration, machines easily, lowest cost. |
| Ductile iron | QT450 / QT500 | When the duty is cyclic or the part takes shock. Tougher than grey. |
| WCB carbon steel | ASTM A216 WCB | Higher strength, weldable. For pressure-bearing bodies. |
| CF8M stainless | ASTM A743 CF8M | Chloride and corrosion duty — the cast equivalent of 316. |
What to Send Us
These are the ones specific to this part. A drawing, a 3D file or the worn original covers all of them at once.
| Item | Why it matters |
|---|---|
| Impeller diameter and clearance | Sets the chamber steps — the one dimension that makes it scrap if it is wrong |
| Top port thread | BSP, NPT or metric, and which way the outlet faces |
| Foot bolt pitch | Decides whether it drops onto the base plate you already have |
Related Castings
Other parts in the same range — all shown as 3D models you can turn.